
Manufacturing Execution System (MES): Complete Guide for Modern Factories (2026)
In today’s fast-paced industrial environment, manufacturing executives face relentless pressure to boost production throughput, maintain strict quality control, and reduce operational waste. While high-level corporate software manages customer orders, purchasing, and business financials, a significant visibility gap often exists on the plant floor itself. Bridging the gap between high-level business strategy and physical shop-floor execution requires a specialized digital backbone: the Manufacturing Execution System (MES).
An MES acts as the dynamic control center for modern manufacturing operations. By connecting machinery sensors, operator terminals, and enterprise management software, it provides real-time visibility into active work orders, asset health, material usage, and quality control metrics. In this complete guide, we will explore what an MES is, how it functions, its essential features, implementation challenges, and how it compares directly with ERP, MRP, and SCADA architectures.
Table of Contents
- What Is a Manufacturing Execution System (MES)?
- Why Manufacturers Need an MES
- How a Manufacturing Execution System Works
- Key Features of a Manufacturing Execution System
- Benefits of Implementing MES
- MES vs ERP: What’s the Difference?
- MES vs MRP
- MES vs SCADA
- Architecture Comparison Table
- Industries That Commonly Use MES
- Common MES Implementation Challenges
- Best Practices for Successful MES Implementation
- Frequently Asked Questions
- Conclusion
What Is a Manufacturing Execution System (MES)?
A Manufacturing Execution System (MES) is an integrated software platform that monitors, tracks, documents, and controls the transformation of raw materials into finished goods in real time on the factory floor. Sitting between high-level enterprise planning systems and physical shop-floor machinery, an MES provides real-time operational data, allowing plant managers to optimize manufacturing processes as they occur.
According to international manufacturing standards, an MES delivers vital functional capabilities across eleven core areas, including finite resource scheduling, dispatching work units, product tracking, quality management, and labor management. By replacing manual paper logs with automated data capture, a Manufacturing Execution System creates an agile environment where operational issues are identified and resolved immediately.
Why Manufacturers Need an MES
Without a dedicated Manufacturing Execution System, plant operators must rely on manual spreadsheets, paper travelers, and end-of-shift reporting. This delayed data flow creates operational blind spots, making it impossible to catch equipment bottlenecks, material shortages, or quality deviations as they happen.
Implementing an MES provides continuous, real-time visibility across the shop floor. It allows industrial organizations to eliminate manual data entry errors, enforce standardized operating procedures, lower product defect rates, and ensure full compliance with regulatory standards. Effective execution tracking directly strengthens overarching Production Planning in Manufacturing workflows by ensuring plans are executed reliably on the shop floor.
How a Manufacturing Execution System Works
A modern Manufacturing Execution System operates as an interactive communication engine, gathering data from human operators, Programmable Logic Controllers (PLCs), IoT machine sensors, and enterprise software platforms. It translates raw operational signals into actionable insights through five structured functional stages:
Production Planning Integration
The MES automatically receives released work orders, Bills of Materials (BOMs), and master schedules directly from enterprise software. It breaks these macro plans down into granular, station-specific dispatch lists for immediate execution.
Shop Floor Data Collection
As production begins, the software captures live operational data through connected IoT sensors, barcode scanners, PLC interfaces, and operator terminals. It automatically records cycle times, machine speeds, material consumption, and downtime events.
Real-Time Monitoring
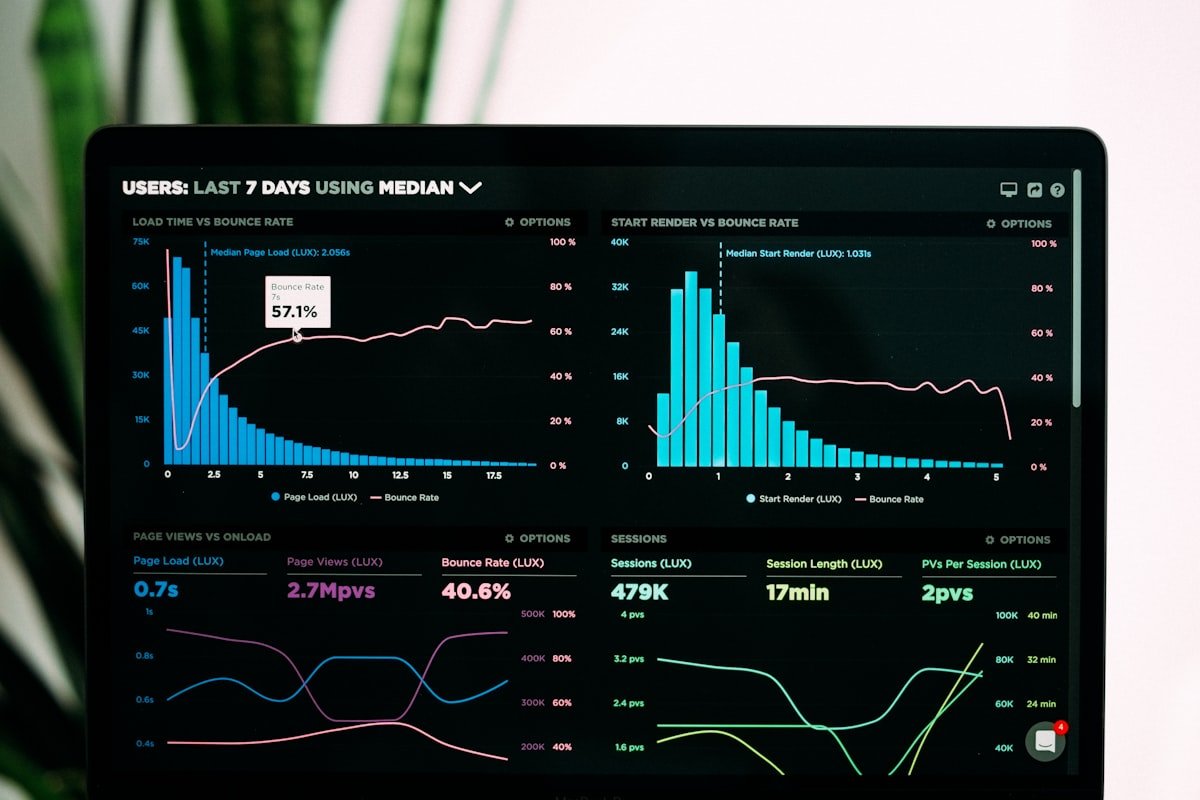
The system constantly compares live shop-floor performance against established baseline targets. If a machine slows down, experiences an unplanned breakdown, or generates defective parts, the system alerts operators and supervisors instantly via visual dashboards.
Quality Management
Integrated quality checkpoints enforce inline inspections. The MES records dimensional measurements, test results, and operator observations, automatically quarantining out-of-spec batches before they move further down the assembly line.
Production Reporting
At the end of a shift or job run, the system generates comprehensive performance summaries. These reports calculate key productivity metrics, track material consumption, and document complete product genealogy records for future reference.
Key Features of a Manufacturing Execution System
Leading digital platforms provide a comprehensive set of features engineered to optimize every aspect of shop-floor operations:
Production Scheduling
Dynamic finite-capacity scheduling tools allow plant dispatchers to sequence work orders based on real-time machine availability, tooling constraints, personnel qualifications, and job priorities.
Work Order Management
Digital work order management routes jobs through required work centers, supplying operators with digital work instructions, engineering drawings, and safety checklists right at their workstations.
Machine Monitoring
Direct integration with machine controllers provides real-time tracking of asset operational states, operational speeds, temperature profiles, and unscheduled downtime reasons.
Inventory Tracking
The system tracks raw material movement, WIP staging, and finished goods creation in real time. Maintaining precise WIP visibility works hand-in-hand with robust Manufacturing Inventory Management practices.
Quality Control
Automated Statistical Process Control (SPC) modules evaluate quality parameters during active production runs, triggering immediate corrective action workflows when process drift occurs.
Traceability & Genealogy
Complete product genealogy logs capture raw material lot numbers, equipment usage history, environmental conditions, and testing results for every manufactured unit. This level of detail is vital for regulatory compliance and efficient recall management.
Performance Analytics
Built-in analytics engines process raw operational telemetry into standardized operational metrics, giving managers live visibility into floor performance. You can explore essential metrics in our guide on 15 Manufacturing KPIs Every Factory Should Track.
Benefits of Implementing MES
Deploying a robust Manufacturing Execution System delivers significant financial, operational, and strategic benefits across manufacturing organizations:
Increased Production Efficiency
By eliminating manual paperwork, optimizing job dispatching, and minimizing machine downtime, facilities increase overall throughput without purchasing extra capital equipment.
Improved Product Quality
Enforcing inline quality checks prevents defective components from continuing through assembly. Catching defects early reduces scrap rates, rework costs, and warranty claims.
Reduced Manufacturing Costs
Real-time tracking highlights energy waste, labor inefficiencies, and excessive material scrap. Eliminating these inefficiencies is a core component of sustainable Manufacturing Cost Control strategies.
Better Inventory Visibility
Tracking material consumption in real time eliminates buffer stock hoarding and prevents unexpected component shortages. Precise floor tracking supports streamlined Warehouse Management in Manufacturing workflows.
Faster Decision Making
Visual dashboards deliver live performance metrics directly to supervisors, replacing delayed end-of-day reports with immediate, data-driven decision-making capabilities.
Regulatory Compliance
Automated genealogy logs simplify compliance auditing for regulated industries by creating searchable electronic batch records (eBRs) and device history records (DHRs).
MES vs ERP: What’s the Difference?
While both systems are critical to modern industrial enterprises, they operate at different architectural layers and serve distinct operational goals:
- Enterprise Resource Planning (ERP): Manages high-level business functions over weeks, months, or quarters. It handles financial accounting, procurement, sales order management, human resources, and high-level master scheduling. To learn more about enterprise systems, read our foundational guide on What Is Manufacturing ERP?.
- Manufacturing Execution System (MES): Manages shop-floor execution in real time (seconds, minutes, and shifts). It focuses directly on machine control, job dispatching, WIP tracking, and quality assurance. For additional software insights, review our article on the Top 10 Benefits of ERP in Manufacturing.
MES vs MRP
Material Requirements Planning (MRP) systems focus primarily on inventory calculations and material ordering timelines based on sales forecasts. In contrast, an MES manages actual physical shop-floor execution, tracking component consumption as jobs move through assembly lines. For a deeper look at planning software differences, explore our analysis of ERP vs MRP.
MES vs SCADA
Supervisory Control and Data Acquisition (SCADA) systems operate at the machine control layer, focusing on direct equipment monitoring, alarm processing, and automated process adjustments. An MES sits directly above SCADA, translating technical machine signals into broader operational metrics like job status, work order progress, and labor allocation.
Architecture Comparison Table
The table below summarizes the primary functional differences across core industrial software layers:
| Functional Feature | MES (Execution) | ERP (Enterprise) | MRP (Materials) |
|---|---|---|---|
| Shop Floor Monitoring | ✅ Real-Time (Seconds/Minutes) | ❌ No Direct Control | ❌ No Direct Control |
| Production Scheduling | ✅ Detailed Finite Scheduling | Limited High-Level Master Plan | Limited Time-Phased Plan |
| Inventory Planning | Limited (WIP Focus) | ✅ Enterprise Inventory | ✅ Material Requirements |
| Financial Management | ❌ No Financial Accounting | ✅ Full Financial Ledger | ❌ No Financial Ledger |
| Real-Time Machine Data | ✅ Direct Sensor/PLC Integration | ❌ No Direct Integration | ❌ No Direct Integration |
| Quality Management | ✅ Inline SPC & Defect Capture | Limited Post-Process Log | ❌ No Quality Tracking |
Industries That Commonly Use MES
A Manufacturing Execution System provides value across diverse manufacturing environments, particularly in sectors requiring strict quality control and full product traceability:
Automotive
Automotive OEMs and Tier-1 suppliers use software to manage complex, multi-option assembly lines, track component serial numbers, and verify error-proofing sequences across fast-paced production lines.
Food & Beverage
Food processors rely on software to manage recipe execution, monitor mixing temperatures, track batch expiration dates, and ensure rapid traceability during product recall events.
Electronics
High-tech electronics manufacturers utilize software platforms to track surface-mount technology (SMT) lines, record component lot numbers, and enforce strict electrostatic discharge (ESD) quality testing protocols.
Pharmaceuticals
Pharmaceutical manufacturers require validated software platforms to enforce electronic batch records (eBR), maintain cGMP regulatory compliance, and prevent contamination across cleanroom environments.
Aerospace
Aerospace manufacturers use specialized platforms to manage long cycle-time assembly runs, enforce tight machining tolerances, and maintain complete structural material histories for aircraft components.
Common MES Implementation Challenges
While the benefits are clear, deploying a Manufacturing Execution System requires careful planning to overcome common operational hurdles:
Employee Resistance
Shop-floor operators accustomed to paper-based processes may resist adopting new digital tools or feel micro-managed by real-time tracking systems. Clear communication and early involvement are essential to build buy-in.
Legacy System Integration
Connecting modern software engines to legacy shop-floor equipment lacking digital communication capabilities often requires installing third-party IoT sensors or edge hardware interfaces.
Data Accuracy
An execution platform relies entirely on accurate input data. If operators fail to log setup times or scrap reasons correctly, system reports become unreliable, undermining decision-making.
Training Requirements
Comprehensive training programs must be conducted across all shifts to ensure operators, supervisors, maintenance technicians, and quality inspectors can navigate the system confidently.
Best Practices for Successful MES Implementation
To maximize your return on investment and ensure a smooth rollout, follow these established industry deployment practices:
- Define Clear Project Objectives: Identify specific operational pain points—such as high scrap rates or poor OEE—and establish measurable target KPIs before selecting software.
- Involve Shop Floor Teams Early: Include machine operators and line supervisors in software configuration design to ensure system interfaces are intuitive and practical.
- Standardize Processes First: Do not digitize inefficient, broken processes. Clean up physical shop-floor routines and standardize workflows before software deployment.
- Adopt a Phased Rollout: Pilot the platform on a single production line or work center first. Refine configurations and incorporate feedback before expanding across the facility.
- Align with Recognized Standards: Structure system architectures around recognized frameworks from organizations like MESA International, ISA (International Society of Automation), and the NIST – Smart Manufacturing initiative.
Frequently Asked Questions
What is the primary purpose of an MES?
The primary purpose of a Manufacturing Execution System (MES) is to monitor, track, and control shop-floor manufacturing operations in real time. It converts released sales orders into finished goods while optimizing equipment efficiency, material tracking, and product quality.
Is MES the same as ERP?
No. An ERP system manages macro-level enterprise business functions—such as finance, procurement, and high-level master schedules—over longer time horizons. An MES controls minute-by-minute execution on the physical factory floor, managing machines, operators, work instructions, and quality checks.
Can small manufacturers use MES?
Yes. Modern cloud-based platforms make execution systems accessible to small and mid-sized manufacturers. Modular systems allow smaller factories to start with basic machine tracking or digital work instructions and expand functionality over time.
What industries benefit most from MES?
Industries with complex assembly routines, strict quality regulations, or high brand risk benefit most. Key sectors include automotive, pharmaceuticals, aerospace, food and beverage, electronics, and medical device manufacturing.
How much does an MES implementation cost?
Implementation costs vary widely depending on facility size, number of connected machines, deployment model (cloud vs. on-premises), and integration complexity. Cloud SaaS models allow factories to start with lower upfront capital costs through subscription-based pricing.
Conclusion
Deploying a modern Manufacturing Execution System is a foundational step for factories seeking to build agile, data-driven Smart Manufacturing operations. By connecting enterprise software with real-time shop-floor execution, an MES eliminates operational blind spots, reduces production waste, and improves product quality.
When combined with clear operational strategy and integrated enterprise systems, an MES gives plant leadership the visibility needed to drive continuous improvement. Embracing digital execution tools ensures your manufacturing facility stays competitive in a rapidly evolving market.
